
 English
 中文简体
 русский
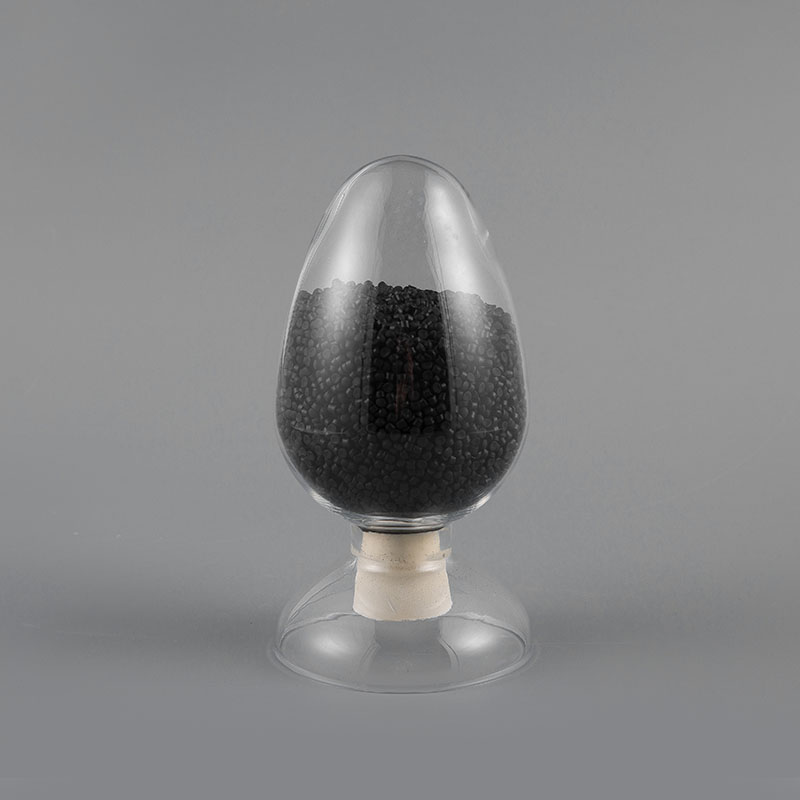
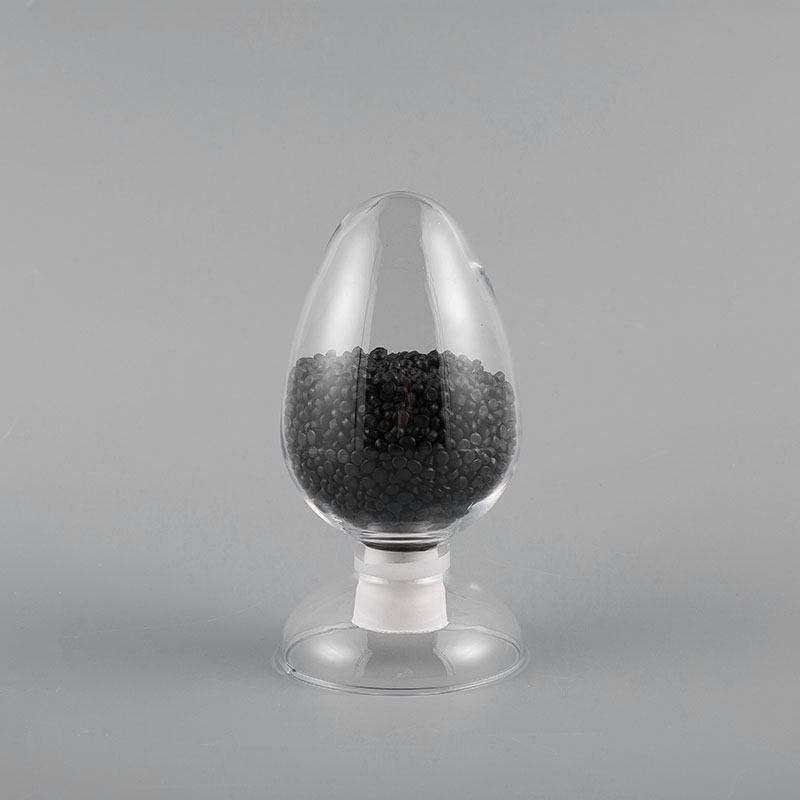
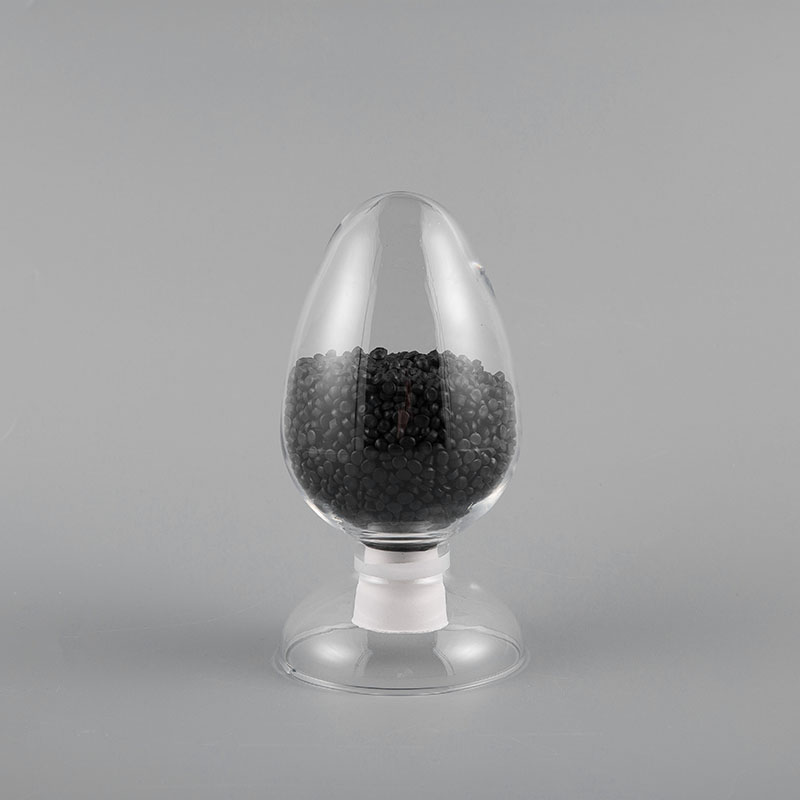
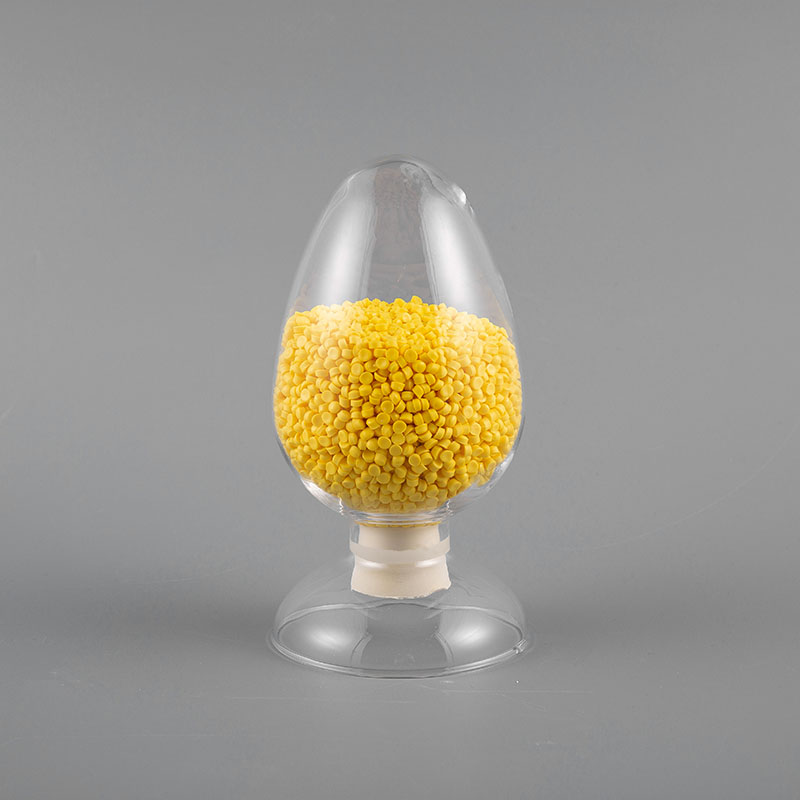
JR-70 70℃ PVC Flame Retardant Flexible Insulation Compound is a high-performance insulation material...
Product Category
Related Products
Elevator Cable Compound Suppliers
-
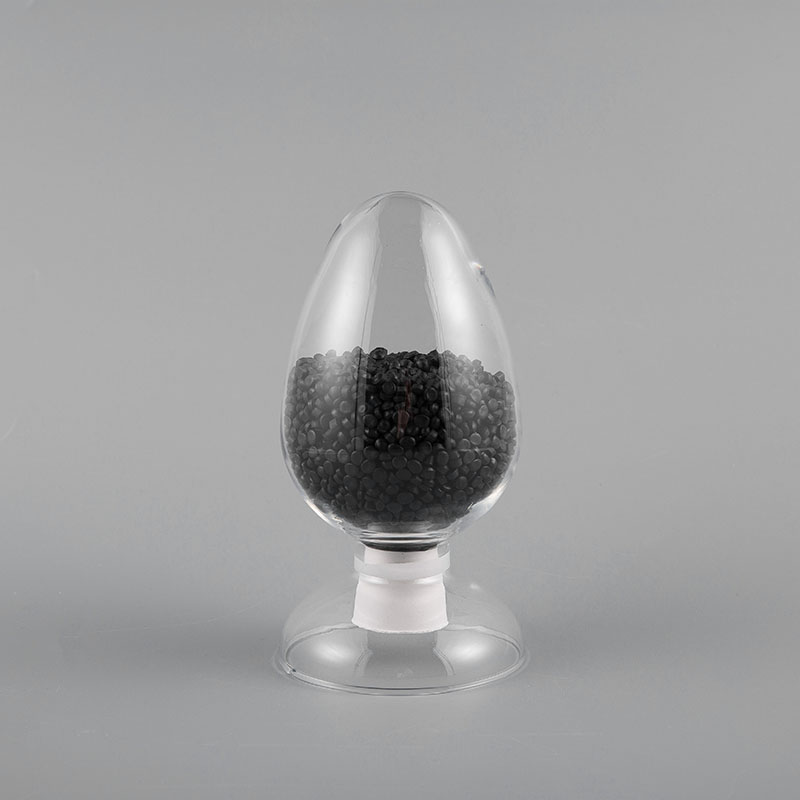
HR-70 70℃ PVC Flame Retardant Flexible Sheath Compound
More DetailsThe HR-70 PVC Flame Retardant Compound is a specialized pelletized material designed for the extrusi...

ABOUT US
30YEARS OF
EXPERIENCE
About Us
Coming From China, Marketing To The World.
Hangzhou Meilin New Material Technology Co., Ltd. is China ODM/OEM Elevator Cable Compound Suppliers and Wholesale Elevator Cable Compound, we were established in July 1994 (formerly known as Zhejiang Lin'an Hongyan Plastic Factory). The company has two factories located at 619 Linglongshan Road and 259 Xingyu Street, Lingqiu Street, Linglong Industrial Park, Lin'an District, Hangzhou City. The registered capital of the company is 75 million yuan, covering an area of over 18000 square meters and a building area of over 30000 square meters. Currently, modern industrial factories and 18 advanced automated production lines have been built. The new factory area will be produced in 2021, making it the cleanest and most beautiful professional cable material manufacturer in the entire region—agreement conditions.
Honor
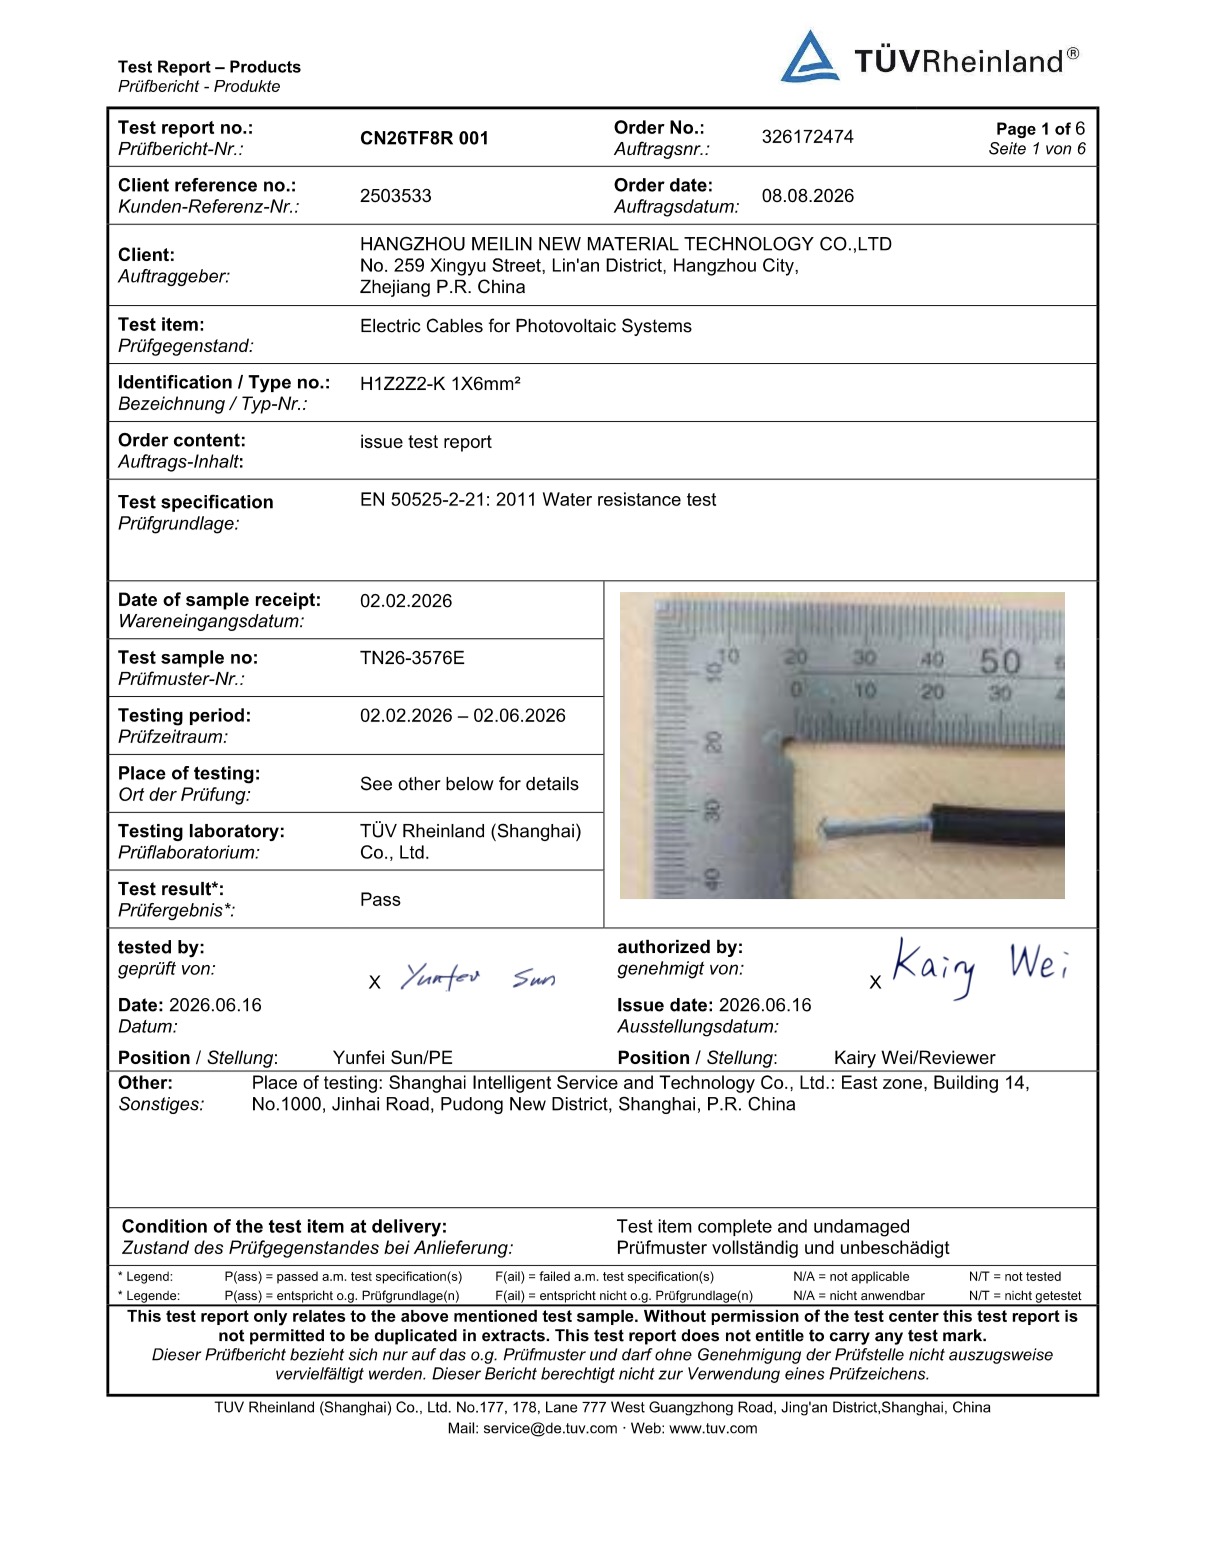
Certifications
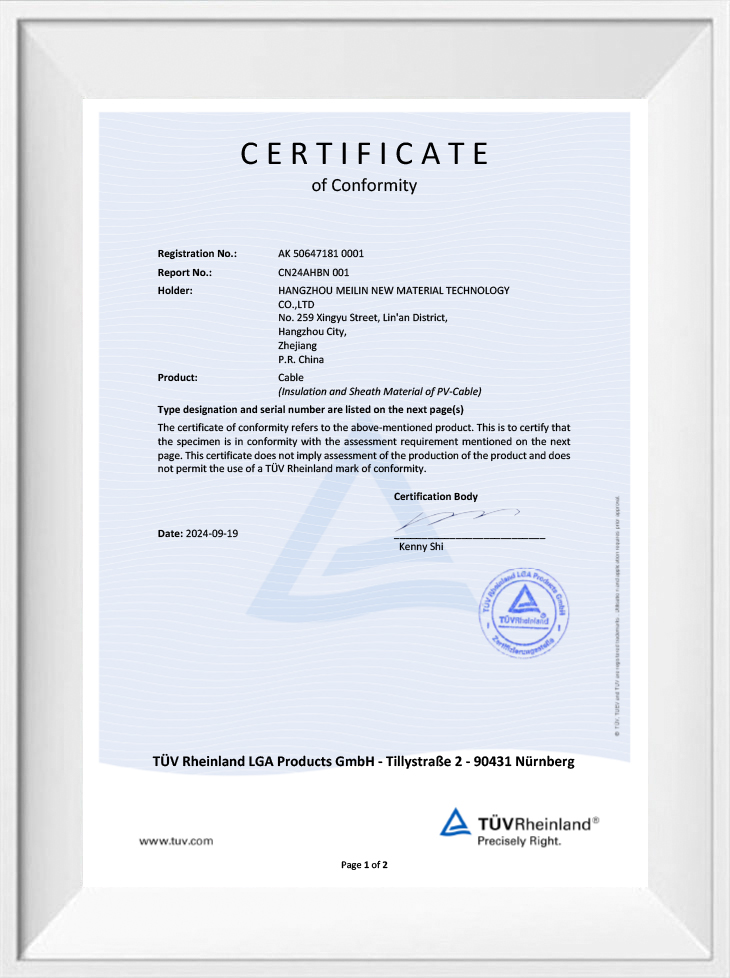
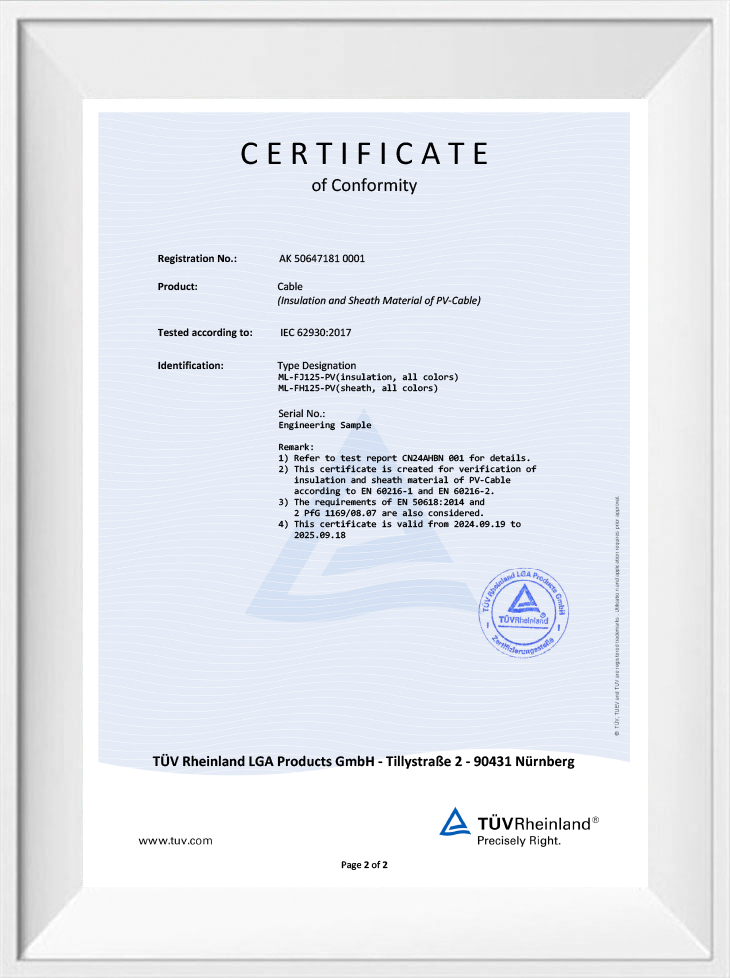
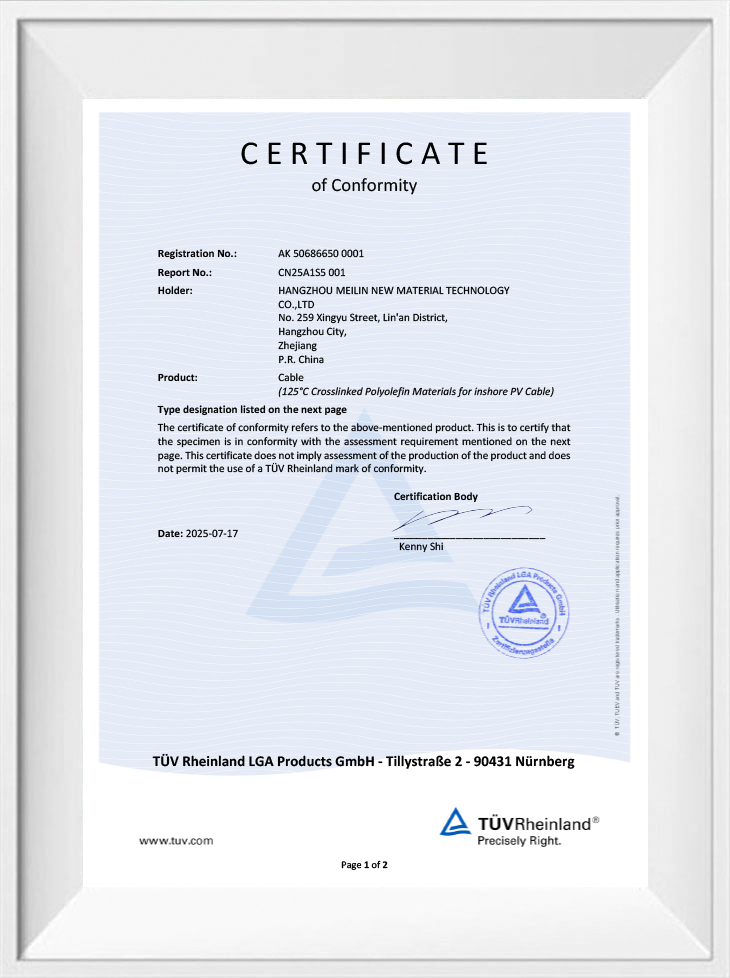
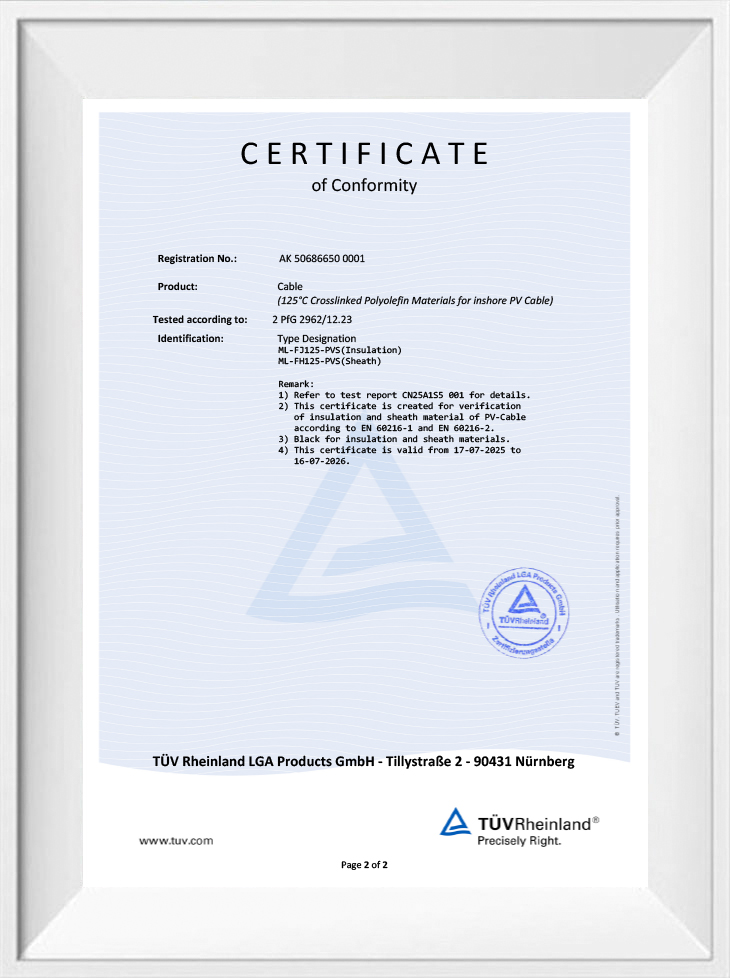
News
-
admin 20 Nov 2026
Automotive Wire Compounds: How to Evaluate Heat Resistan...
Read MoreCompound Evaluation Guide A 105 °C PVC automotive wire compound can pass a 240-hour oven test and still crack inside a transmission tunnel after 3,000 hours at the same nominal temperature. The diffe...
-
admin 18 Nov 2026
Custom Wire and Cable Compounds: What to Specify When So...
Read MoreA compound that passes every incoming inspection can still fail on your extruder. The usual cause is not a bad batch. It is a specification that described the pellet instead of the finished cable: a...
-
admin 13 Nov 2026
Water-Resistant Cable Compounds for Underground and Subm...
Read MoreA 33 kV feeder laid in saturated clay and a submarine export cable crossing a tidal landfall fail for the same reason: water reaches the insulation screen. In both cases the decisive choice was made...
-
admin 11 Nov 2026
Medical PVC Compound Performance: Key Factors Guide
Read MoreA Medical Polyvinyl Chloride Compound is not defined by its base resin alone — flexibility, transparency, chemical resistance, and processing behavior all come from the combination of resin grade, pl...
Elevator Cable Compound Industry Knowledge
Fire-Resistant Elevator Cable Compounds: Meeting New Global Safety Standards
The demand for fire-resistant elevator cable compounds has surged as high-rise construction and stringent safety regulations drive innovation in building materials. With new global fire safety standards like EN 50200, IEC 60331, and NFPA 72 requiring enhanced flame retardancy and low smoke emission, manufacturers are developing advanced halogen-free flame-retardant (HFFR) compounds to meet compliance while ensuring optimal performance.
Key Trends in Fire-Resistant Elevator Cable Materials
1. Halogen-Free vs. Traditional PVC Compounds
Historically, PVC-based elevator cable compounds dominated the market due to their cost-effectiveness. However, concerns over toxic smoke emission during fires have shifted focus toward halogen-free elevator cable materials, which offer:
Lower smoke density (≤50% of traditional PVC)
Reduced corrosivity (pH >4.3 per IEC 60754-1)
Higher flame resistance (meeting UL 94 V-0 standards)
A comparative analysis shows that LSZH (Low Smoke Zero Halogen) elevator cables outperform PVC in critical safety metrics:
| Parameter | PVC Compound | HFFR (LSZH) Compound |
|---|---|---|
| Flame Retardancy | UL 94 V-1/V-2 | UL 94 V-0 |
| Smoke Density | High (>80%) | Low (<50%) |
| Toxicity | High HCl emission | Minimal toxic fumes |
| Oxygen Index | 20-25% | >30% |
| Corrosivity | Highly corrosive | Non-corrosive |
2. Silicone-Based vs. Thermoplastic Compounds
Another emerging trend is the use of silicone-coated elevator cables, which provide superior high-temperature resistance (up to 200°C) compared to standard thermoplastic elevator cable compounds. These are ideal for fire-rated elevator systems in extreme environments.
3. Global Compliance & Market Demand
With EU CPR (Construction Products Regulation) and NFPA 70 (NEC) tightening fire safety norms, manufacturers are optimizing elevator cable insulation materials for:
Oxygen Index (OI) >30% (per ASTM D2863)
Vertical flame resistance (IEC 60332-1)
Low toxicity (EN 60754 compliance)
Consulting Information
CONTACT US
05
-
 ADD:
No. 259 Xingyu Street, Lin'an District, Hangzhou City, Zhejiang Province
-
 TEL/FAX:
+86 571 63761139
-

-

-
CONTACT US
CONTACT US Creative project? Let's have a productive talk.
Copyright © Hangzhou Meilin New Material Technology Co., Ltd. All Rights Reserved. Privacy Policy Wholesale Elevator Cable Compound
